


Injection mould tooling explained: key factors, costs and optimisations
Injection mould tooling is the foundation of any successful plastic moulding project. The quality, design and maintenance of the tooling determine part accuracy, production speed and long-term cost-effectiveness.
If you are a design engineer, product developer or procurement manager, understanding the fundamentals of injection mould tooling helps you make better decisions and avoid costly mistakes.
This guide covers the core considerations, from the difference between “mold” and “mould” in industry contexts to tooling materials, manufacturing, costs and maintenance.
Differences between “mold” vs. “mould” in industry contexts
One of the first things you might notice when researching injection mould tooling is the variation in spelling — “mold” versus “mould.” While they refer to the same process, the spelling changes depending on geographical and industry context.
Basically put, “mould” is the preferred spelling in British English and is used widely in the UK, Europe, Australia, and other Commonwealth countries. The spelling of “mold” is more common in American English and is used in the United States, Canada, and many parts of Asia where American technical standards are adopted.
The distinction isn’t just linguistic. Some tooling suppliers may use “mold” or “mould” depending on where they are based or the markets they serve. This matters when sourcing globally because it often signals differences in standards, measurement systems, and sometimes even quality expectations.
For example:
- UK-based toolmakers typically work to metric dimensions.
- US-based manufacturers often use imperial units, which can require conversions if parts are designed in metric.
For engineers and buyers working in global supply chains, being aware of this spelling difference — and the regional standards that come with it — is important for accurate communication, quoting and specification compliance.
Tooling materials and manufacturing
The choice of materials and manufacturing methods for injection mould tooling affects everything from upfront cost to tool lifespan and cycle time efficiency.
Common tooling materials
Tool steel
The most widely used material for production tools. Grades such as P20, H13 and S136 offer varying balances of hardness, corrosion resistance and machinability.
- P20 steel: Pre-hardened, economical, suitable for medium-volume runs.
- H13 steel: High hardness and heat resistance, suited for abrasive or high-temperature plastics.
- S136 stainless steel: High corrosion resistance, ideal for optical components or parts with demanding surface finish requirements.
Aluminium
Lighter and faster to machine than steel, aluminium tooling is an excellent choice for prototypes or low-volume production. It offers faster heat dissipation, which can reduce cycle times, but has a shorter lifespan compared to steel.
Beryllium copper inserts
Often used in specific tool areas to improve thermal conductivity. They help reduce cooling times and improve moulded part consistency.
Manufacturing processes
The manufacturing of injection mould tooling involves multiple precision processes:
- CNC machining: The backbone of toolmaking, offering accuracy down to microns for complex cavities and cores.
- EDM (Electrical Discharge Machining): Allows precise shaping of hard metals and the creation of fine details, sharp corners, and deep slots that are difficult to machine conventionally.
- Polishing and texturing: Tool surfaces are polished to achieve desired part finishes, from mirror gloss to controlled surface textures.
- Heat treatment: Used for hardening steel to extend tool life and maintain dimensional stability under repeated high-pressure injection cycles.
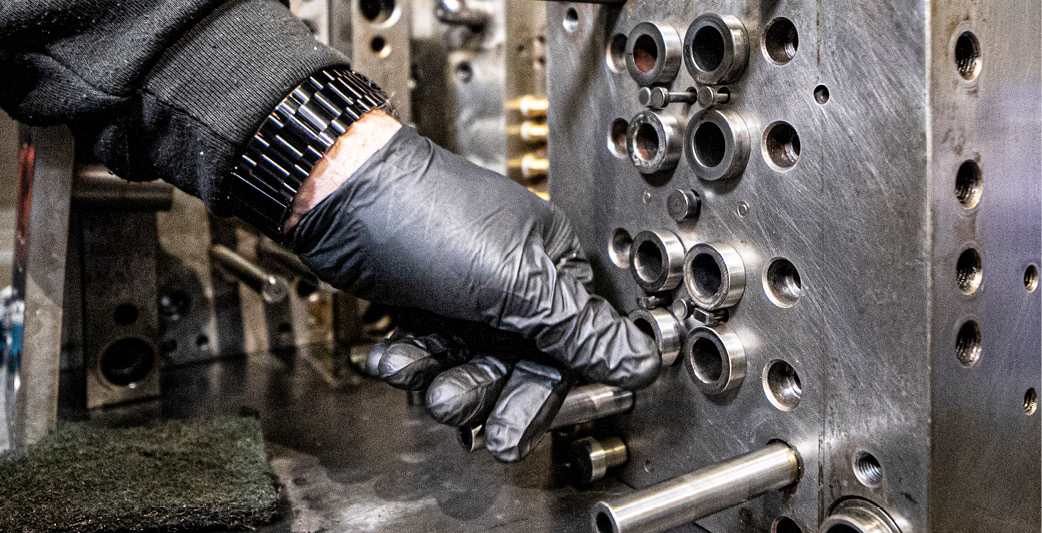
A key part of manufacturing is tool design — the stage where gating, cooling, ejection, and cavity layout are planned. Poor design at this stage can lead to costly production issues such as warpage, sink marks, or flash.
Cost breakdown and ways to reduce tooling expenses
The cost of injection mould tooling can range from a few thousand pounds for simple, single-cavity tools to hundreds of thousands for complex, multi-cavity or multi-material tools.
Factors influencing tooling cost
Part complexity
Parts with undercuts, fine features or complex geometries require additional machining time, side actions, lifters or collapsible cores, which all add cost.
Cavity count
Multi-cavity tools can produce more parts per cycle, reducing cost per part, but they are more expensive to manufacture.
Tool material
Steel tools are more expensive initially but offer longer service life. Aluminium tools cost less upfront but may wear faster.
Surface finish requirements
High-polish or specialist texturing requires skilled labour and can add significantly to costs.
Tolerances
Tighter tolerances require more precise machining, increasing both time and cost.
Ways to reduce tooling expenses
Design for manufacture (DFM)
Simplifying part geometry can remove the need for costly tool features like sliders or lifters.
Standardisation
Where possible, use standard mould base components instead of fully custom designs.
Family tools
If multiple parts can fit into the same tool without quality compromise, this can reduce tooling cost.
Prototype tooling
Use aluminium or soft steel for short runs to validate designs before committing to full production tooling.
Collaborative design reviews
Working closely with the toolmaker early in the design phase can identify cost-saving opportunities before manufacturing begins.
Common tooling issues and maintenance tips
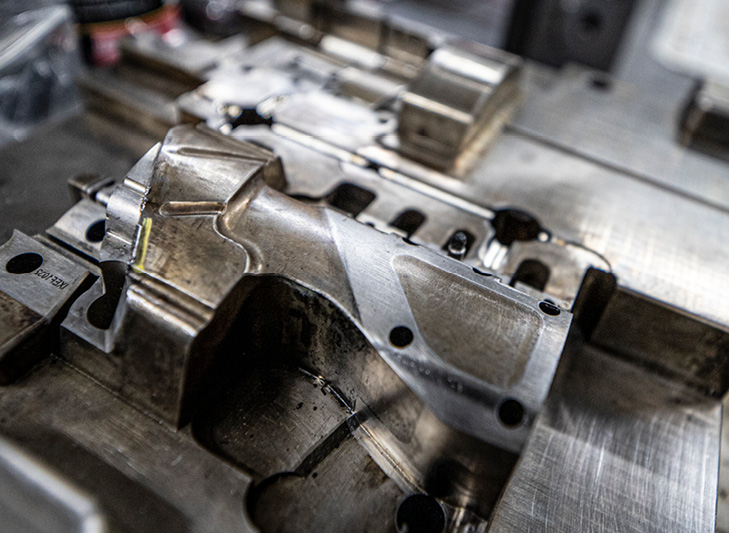
Even the best-designed and manufactured injection mould tooling will require maintenance over its service life. Neglecting maintenance can cause production stoppages, quality issues, and expensive repairs.
Common tooling issues
Flash
Excess plastic that escapes at the parting line. Often caused by tool wear, poor clamp force or incorrect mould alignment.
Burn marks
Dark streaks on the part surface, usually caused by trapped air or degraded material from poor venting.
Short shots
Incomplete filling of the cavity due to inadequate injection pressure, poor gating design or blockages.
Cooling inefficiency
Leads to longer cycle times and warping issues. Often caused by blocked cooling channels or poor thermal conductivity.
Corrosion and rusting
Particularly common when processing hygroscopic materials or in humid environments if the tool is not adequately protected.
Maintenance tips
Regular cleaning
Remove resin build-up, dust, and debris from cavities and vents after each production run.
Lubrication
Keep moving parts such as ejector pins and sliders lubricated to prevent wear and seizure.
Inspection schedules
Periodically check for wear on critical areas like parting lines, gates and cooling channels.
Rust prevention
Apply corrosion inhibitors before storing tools, especially for long-term storage.
Record keeping
Maintain a log of tool use, maintenance and repairs. This helps in predicting when preventative work is required.
Injection mould tooling is both an investment and a performance driver for any plastic moulding project. From the choice of materials and manufacturing processes to the way the tool is maintained, every factor influences cost, part quality and production efficiency.
By understanding regional terminology differences, selecting the right tool materials, applying cost optimisation strategies, and implementing a disciplined maintenance schedule, businesses can maximise the lifespan and efficiency of their tools while reducing long-term production costs.
For companies seeking UK-based injection mould tooling expertise, PMP offers precision manufacturing and lead times you can rely on. Our engineers work with you from design through to production, ensuring your tooling is built to deliver accuracy, speed and value across its entire service life.
To discuss your injection mould tooling requirements, contact PMP today. You can also follow us on LinkedIn for the latest updates.
